Global buyers entering 2026 need more than a supplier’s low defect-rate promise. They need visible, repeatable evidence. Tour-Level Quality Control means connecting design approval, production checks, testing, packaging, and shipment records. The ISO Survey 2023 reported 1,265,216 valid ISO 9001 certificates worldwide. However, certification shows process commitment, not guaranteed product quality. A certificate cannot prevent a wrong color match on Tuesday.
Deloitte’s 2024 Global Chief Procurement Officer Survey identifies resilience, supplier visibility, and risk management as continuing procurement priorities. The World Quality Report 2024–25 also highlights growing artificial intelligence use in quality engineering, with human judgment still essential. These findings matter for buyers comparing factories across different countries, languages, and production cultures. A strong program should combine supplier audits with first-article inspection, approved samples, calibrated gauges, and photographic records. Use ISO 2859-1 sampling carefully. Sampling reduces uncertainty, but it never removes it.
Look for traceability at carton level. Check batch numbers, material certificates, test results, and final inspection dates. Ask who approves a deviation, and how quickly the factory responds. A clean dashboard can still hide weak shop-floor discipline. No checklist is perfect. Experienced buyers should review recurring defects, not only pass-or-fail results. They should also test whether corrective actions remain effective after three production cycles. This introduction examines practical Tour-Level Quality Control methods for global purchasing decisions, while recognizing an uncomfortable truth: the best system still depends on honest data and disciplined people.
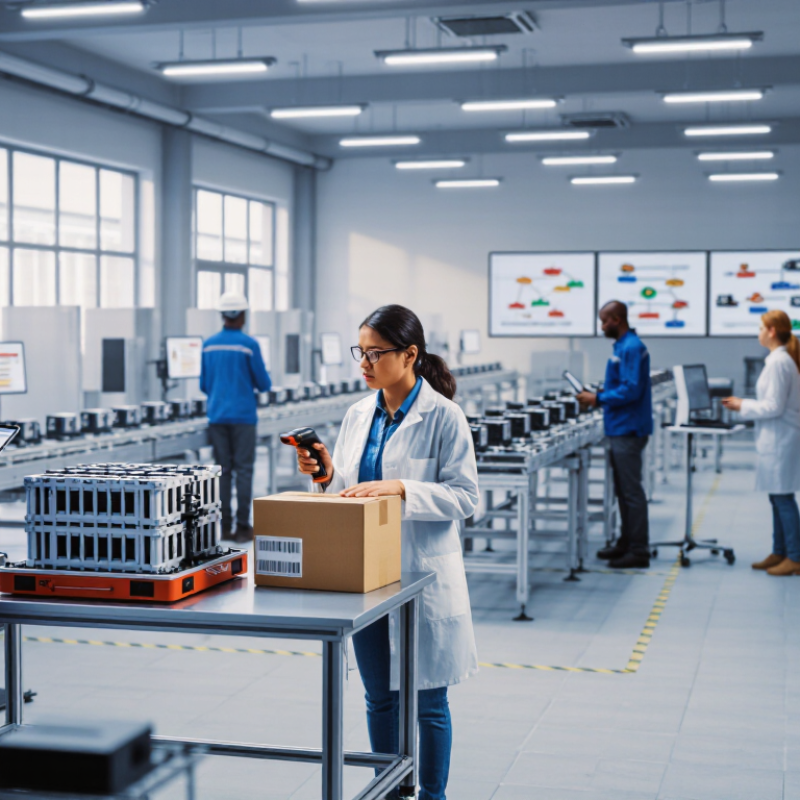
Still, no control plan is perfect. A supplier can meet a sample standard while hiding variation between lots. That uncomfortable possibility requires random audits and trend reviews, not blind trust. One missed defect can expose a weakness. Buyers should study complaint data, corrective-action speed, and whether the same fault returns. Honest reporting may reveal slower production or higher inspection costs. Those findings are inconvenient, but they improve purchasing decisions. Each release should carry a traceable inspection record before shipment approval.
Reliable international sourcing begins with a clear inspection plan, not a rushed factory visit. Define materials, dimensions, performance limits, packaging, and labeling before production starts. Every requirement should be measurable. “Good quality” is too vague.
Use approved drawings, reference samples, and controlled specifications. AQL sampling can support consistent decisions, while critical defects usually require zero acceptance. Inspectors should verify product quantity, workmanship, safety features, and functional performance. They should also check cartons, barcodes, moisture protection, and shipping marks. Small errors often become expensive at the destination.
Keep evidence practical. Record lot numbers, inspection times, test results, and calibrated equipment details. Take clear photos of defects and packaging conditions. Pre-production, in-line, and pre-shipment checks reveal different risks. Do not rely only on final inspection. Too late, sometimes.
A strong report separates critical, major, and minor defects. It identifies the responsible process and requests corrective action with a deadline. Yet sampling is never perfect. A clean sample can hide inconsistent production. Buyers should review repeated findings, supplier responses, and trend data across orders. I would also question my own checklist after every shipment. It may miss real-world handling, unclear instructions, or damage caused during loading. Quality control improves when inspection records become lessons, not just paperwork.
2026 Best Tour Level Quality Control for Global Buyers?
Step-by-Step Quality Control Procedures from Factory to Shipment
Reliable quality control begins with a clear purchase specification. Confirm materials, dimensions, colors, tolerances, packaging, and approved samples before production starts. Factory engineers should review every requirement with the buyer. Unclear details create expensive corrections later. Keep written records.
During production, inspectors check incoming materials and the first completed units. They measure critical points with calibrated tools, not visual judgment alone. A production-line check can reveal loose stitching, uneven coating, wrong labels, or unstable assembly. Inspectors should record photographs, batch numbers, and defect locations. Small defects matter.
Before packing, a final inspection uses a representative sample from finished cartons. The process should include quantity verification, function testing, appearance checks, carton strength, and shipping marks. Random sampling is useful, but it cannot replace risk-based testing for critical components. Separate failed units immediately. Do not hide them inside rework piles. One missed variation in shade or size can affect an entire shipment. That weakness deserves review. After approval, confirm pallet condition, container cleanliness, loading records, and seal numbers. Quality control ends with evidence, not a verbal promise.
2026 Best Tour Level Quality Control for Global Buyers?
Reliable global quality verification begins with evidence, not confident promises. Experienced inspectors should work from approved specifications, drawings, samples, and measurable acceptance criteria. Each inspection needs a clear record of quantity, batch identification, production stage, and inspection location. A simple checklist is useful, but it cannot replace judgment.
Digital tools can strengthen this process. Inspectors may use calibrated gauges, timestamped photographs, video calls, and secure cloud records. Data should connect each finding to a product lot and inspection point. This creates a traceable evidence chain for buyers, suppliers, and independent reviewers. Automated reports also reduce transcription errors. They do not remove human responsibility.
Small details matter. A photo should show the defect scale, not only the defect. Measurement units must remain consistent across countries. Documents should state who inspected, when, and under which procedure. Translation needs technical review, especially for tolerances and safety requirements. No system is perfect. A missed surface flaw can still pass through a well-designed process. That failure should trigger a documented review, not quiet deletion. Teams should compare inspection results, revisit sampling plans, and record corrective actions. Reliable verification grows through honest evidence, repeatable methods, and the willingness to question convenient results.
Tour-level production leaves little room for late surprises. Products must survive repeated handling, tight schedules, and international delivery. A suitable quality control partner needs more than basic inspection skills. They should understand production pressure and protect measurable quality standards.
Look for inspectors with factory experience, trained measurement methods, and clear reporting systems. Before production starts, share approved samples, drawings, packaging details, and critical tolerances. During inspection, the team should check materials, workmanship, dimensions, function, labels, and carton strength. Photos should show defects clearly, not merely confirm attendance. Reports must identify root causes and practical corrective actions.
Ask how the partner manages independence. An inspector should report defects directly, even when a factory requests approval. Check whether they can perform pre-production, in-line, and final inspections across different regions. Their sampling method should match product risk, order value, and delivery urgency. One fixed checklist is rarely enough.
I have seen minor stitching errors become costly shipment delays. Small gaps can matter. Still, no inspection plan is perfect. Measurement tools may drift, samples may hide variation, and rushed reviews can miss patterns. A reliable partner welcomes questions, records limitations, and improves the inspection plan after each production cycle. That honesty is more useful than a flawless-looking report.
Newsletter SignupUpcoming events, promo offers, member exclusives and more.
Golf Fanatics is a Chrysalis Enterprises Company owned by a group of like-minded individuals who share a common passion and affinity for golf, investing in successful Small-Medium-Enterprises, creating rewarding employment opportunities and being good industry participants and corporate citizens.
Monday
Tuesday
Wednesday
Thursday
Friday
Saturday
Sunday
9 a.m. – 10 p.m.
8 a.m. – 10 p.m.
8 a.m. – 10 p.m.
8 a.m. – 10 p.m.
8 a.m. – 11 p.m.
8 a.m. – 11 p.m.
8 a.m. – 9 p.m.
Copyright © 2025 · Golf Fanatics is a division of Chrysalis Golf Ventures Inc.
7100 15th St SE, Calgary AB
This site is protected by reCAPTCHA and the Google Privacy Policy and Terms of Service apply.
Need help? Call our support 24/7

Just a few things before you book…
While Toptracer Range technology and our automated ball dispensers are 99% reliable, there are rare instances when they do not function properly, especially during periods of inclement weather.
Please note that we do not guarantee the reliability of these services during any booking and will not provide you with a refund or credit if they do not function properly during your booking, therefore booking our services is fully at your discretion.
By booking our services, you acknowledge full responsibility for the cost of any intentional or unintentional damages to any Golf Fanatics or neighboring property and equipment caused by you or your guests during your booking.
You and your guests hereby agree to indemnify Golf Fanatics from any liabilities associated with any personal injury incurred by you or your guests during your booking.


